
Technical Information – FF ELMAX Core
Datasheet version: 09/2026
Composition
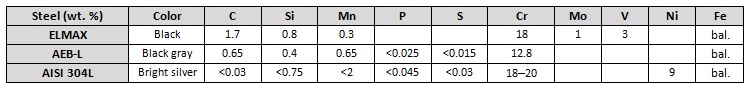
FF Elmax Core is a san-mai stainless damascus steel. A hard Elmax SuperClean core is sandwiched between outer layers of AEB-L and AISI 304L stainless steel, which create a high-contrast pattern once etched. Elmax SuperClean is a martensitic powder-metallurgy stainless steel with a fine, uniform grain structure. It combines high edge retention with high wear and corrosion resistance, which makes blades durable and easy to maintain.
Machining conditions
Our billets are supplied soft-annealed to achieve optimal machinability, with a hardness of approximately 280 HV. You can use all conventional machining methods. Avoid cutting or shaping the material with mechanical shears. We recommend bandsaw cutting, milling, laser cutting, or waterjet cutting. The core thickness increases slightly from the center of the billet toward its edges. For optimal core centricity, position the cutting edge of the blade at the outer rim of the billet.
- Milling – solid carbide mill: Vc 50–60 m/min (164–197 SFM)
- Hard-milling (sizing), solid carbide mill: up to Vc 100 m/min (up to 328 SFM)
- Milling indexable-insert mill: Vc 75–100 m/min (246–328 SFM)
- Milling with HSS-Co mill: Vc 14–16 m/min (46–52 SFM)
- Drilling – HSS-Co drill: Vc 10–12 m/min (33–39 SFM)
- Drilling – PVD coated carbide drill: Vc 60–80 m/min (197–262 SFM)

Grinding
The steel can be ground on all conventional grinders. We recommend belt grinders or Berger grinding machines. For belt grinders, we recommend ceramic-grain belts such as 3M Cubitron II, although conventional abrasives from other manufacturers, for example, SAIT, Klingspor, Norton, or VSM, can also be used. Avoid overheating the steel while grinding. Excessive heat can temper the steel and reduce its hardness.
Soft annealing /
Annealing is only necessary if the material will be further reforged. In that case, the steel structure and properties cannot be guaranteed. Procedure:
- Protect the material from oxidation and heat in a furnace to 980 °C / 1796 °F
- Hold at the temperature for at least 2 hours
- Cool slowly in a furnace to 850 °C / 1562 °F at a rate of 20 °C / 36 °F per hour
- Hold at the temperature for 10 hours
- Continue cooling slowly in the furnace to 750 °C / 1382 °F
- Remove the material from the furnace and allow it to cool slowly in air
Hardening
Hardening is essential to achieve full corrosion resistance and the final hardness of the steel. It must be carried out by
a professional company using vacuum furnaces, such as Bodycote. Recommended process:
- Preheating range: 600–850 °C / 1112–1562 °F
- Austenitizing temperature: 1050–1100 °C / 1922–2012 °F
- Holding time: 30 minutes
- Quenching: gas (nitrogen, overpressure approx. 2 bar) down to approx. 50 °C / 122 °F; quenching in an oil or salt bath is also possible
- Cryogenic treatment: immediately after quenching, at −150 to −196 °C / −238 to −321 °F for 1–3 hours; recommended, increases hardness by approx. 1–3 HRC
If the heat-treatment fails, the material can be re-hardened only once. Repeated re-hardening degrades the material.
Tempering
Tempering must begin as soon as possible, no later than one hour after the hardening process.
- For knife blades, we recommend two tempering cycles of 2 hours each at 200 °C / 392 °F
- To keep blade toughness, we recommend a minimum tempering temperature of 180 °C / 356 °F

Etching
Etching is necessary to bring out the contrast between the layers. You can experiment with various etching techniques depending on your skill level. The steps below describe a method that gives good results.
- Make sure the blade surface is smooth, clean, and free of scratches. Finish it to at least 1000 grit or polish it. Etching does not hide imperfections; it emphasizes them.
- Degrease the blade thoroughly. Washing it in soapy water works well.
- Before etching, test the solution on a sample piece of heat-treated material.
- Before immersing the blade, check the surface of the solution for dirt.
- After etching, neutralize the blade using Na₂CO₃ (sodium carbonate) or NaHCO₃ (baking soda). Alternatively, wash off the etching residue thoroughly with soapy water.
- Dry the etched blade properly. We recommend spraying the blade with WD-40 or a similar product and wiping it dry again.
- For enhanced contrast, lightly polish the etched blade on a buffing wheel. Test this on a sample piece first.
Notes:
- The etching solution can be reused multiple times.
- To make your etching solution more reactive, increase its temperature or FeCl₃ concentration, or add vinegar.
- Do not use automatic stirrers or shaking baths during etching.
- When etching, wear appropriate protective equipment and follow the supplier’s safety data sheet.

Marking
FF ELMAX Core
@futuronforge #HardCOREfuturon #FFELMAXcore
Adresa
Futuron Forge s.r.o.
EU – Czech Republic
Tržiště 372/1
118 00 Praha
IČ: 08244189
DIČ: CZ08244189